Free Consultation :
WHY QX
A supplier may have a large foundry, modern equipment and years of experience. That does not automatically mean the supplier is suitable for your casting.
A foundry capable of producing a 500 kg industrial casting may not be the right foundry for a high-volume D400 ductile iron manhole cover.
A supplier producing EN 124 castings may not automatically be suitable for AS 3996 requirements.
A supplier may have the correct furnace but inadequate sand control.
A supplier may produce good trial castings but struggle with serial production.
A supplier may pass final inspection while having weak process control.
ON THE GROUND
From outside India, it can be difficult to see:
How the supplier actually melts metal
Whether chemistry is consistently controlled
How sand parameters are maintained
Whether patterns are properly maintained
How cores are produced
How gating and risering are controlled
What happens during production delays
How rejected castings are handled
Whether corrective actions are genuinely implemented
Whether production capacity exists when your order arrives
Whether reported production status reflects reality
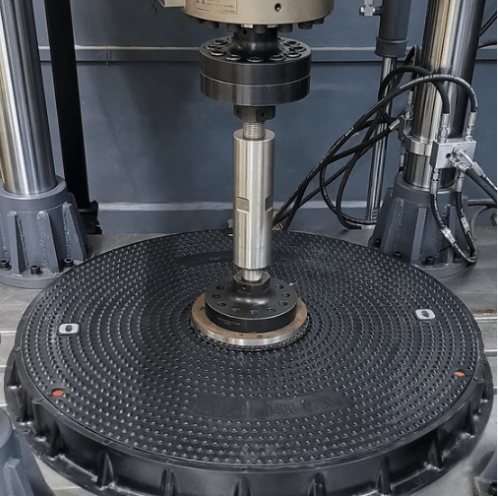
We verify the manufacturing reality behind the supplier’s presentation.
A list of 100 foundries is not supplier intelligence.
QX develops a product-specific understanding of:
The objective is not to give you more supplier names.
The objective is to identify suppliers that make technical sense for your requirement.
WHO WE ARE
QX is built around practical foundry knowledge. A casting is not created at final inspection. It is created through:
Every stage can affect the final product. That is why QX looks beyond the final dimensions.
Pattern
Core
Mould
Metal
Gating
Riser
Solidification
Fettling
Machining
Inspection
Materials: Ductile iron, grey cast iron, GJS grades and GJL grades.
Controls: Carbon/silicon balance, magnesium treatment, inoculation and nodularity.
Checks: Matrix structure, hardness, mechanical properties and chemical verification.
Induction furnace, melt practice and sand parameters.
Moulding systems, automated moulding lines and core-making.
Pattern and tooling, fettling and casting finishing.
Manufacturability review, gating design and riser configuration.
Metal flow, solidification, casting simulation coordination and section thickness.
Machining allowance, draft and core design.
Dimensional verification, gauge mapping and material verification.
Metallography, mechanical testing, load testing, permanent set and visual inspection.
Defect investigation and corrective action.
THE DRAWING DEFINES THE REQUIREMENT.
THE PROCESS DETERMINES WHETHER THE REQUIREMENT BECOMES REALITY.
Evidence Before Assumption. Process Before Paperwork. Technical Facts Before Excuses.
WHY CASTINGS?
They may look simple. Manufacturing them consistently is not.
The final product depends on every step in the chain:
Material
Melting
Chemistry
Treatment
Sand
Moulding
Core
Pattern
Gating
Risering
Solidification
Fettling
Machining
Inspection
Testing